Shot Blasting Machine Belt Maintenance: How to Store, Clean, and Install It
Shot blasting machine belt maintenance starts before the belt is fitted and continues until the day it is replaced: store it cool, dry and well supported, keep trapped shot off the belt and rollers, check the edges, perforations and guide rib on a routine, install it by its guide structure and running direction, and order the next belt at the first clear sign of wear.
This guide applies to the rubber tumble belts used in tumble-type shot blasting machine belts and rubber tracks. Always combine it with the machine manufacturer’s procedure.
How to store a shot blasting machine belt
Rubber products can deteriorate before installation when exposed to ultraviolet light, ozone, heat, moisture, chemicals, or sustained deformation. Store the belt indoors in a cool, dry area and keep its original protective packaging in place where practical. Stored this way, a finished tumble belt can be kept for a long time before it is fitted.
Keep the belt away from light and heat
- Store indoors and out of direct sunlight.
- Avoid strong artificial light with high ultraviolet output.
- Keep the belt away from heaters, boilers, and hot pipework.
- Follow the supplier’s storage-temperature range because acceptable conditions depend on the rubber compound and packaging method.
Control ozone, moisture, and chemicals
- Keep the belt away from high-voltage or sparking electrical equipment that may generate ozone.
- Protect it from rain, floor moisture, oils, fuels, acids, alkalis, solvents, and corrosive liquids.
- For longer storage, use an opaque protective cover that does not trap moisture against the belt.
Prevent deformation and handling damage
- Use a wide, smooth support so the belt is not sharply folded or locally compressed.
- Do not drag the belt or lift it with a narrow hook that may cut the rubber or reinforcement.
- Do not place heavy parts on top of the belt.
- Retain the product label, drawing number, running-direction mark, and inspection record.
Packaging should match how long the belt will wait and how it will be handled. Hongkun ships tumble belts in wooden crates or woven wrapping, chosen to suit the customer’s transport and storage plan. If the spare belt will sit in a warehouse for months, a crate gives better protection against crushing and stacking.
Before installation, inspect both surfaces, edges, perforations, molded ribs, and any splice or joint. Isolate a belt with cracking, hardening, swelling, cuts, exposed reinforcement, flattened guide ribs, or shipping deformation for supplier review.
How to clean and inspect the belt
Cleaning removes trapped abrasive and metal fragments that can repeatedly cut the rubber and keeps the perforations open for the abrasive-return function intended by the machine design.
Routine cleaning on the machine
- Lock out the machine and allow every rotating part to stop.
- Remove loose abrasive, scale, and metal fragments with an industrial vacuum or a soft, non-metallic brush.
- Clear perforations without forcing sharp debris into the reinforcement. Use an approved blunt tool and never enlarge the holes.
- Inspect belt edges, the inner surface, guide rib, roller grooves, end discs, liners, and shot-trap areas.
- If wiping is needed, Hongkun recommends a neutral water-based detergent at pH 6.5–8.0, or warm water no hotter than 40°C (104°F), applied with a soft cloth.
- Keep liquid away from bearings, seals, motors, sensors, electrical components, and enclosed areas. Air-dry completely before operation.
Removing grease and persistent contamination
Use a rubber-safe neutral degreaser for heavy grease. Isopropyl alcohol (IPA) may be used only for quick, localized spot-wiping followed by immediate air drying. Do not soak the belt or leave IPA on its surface.
Inspect a new or removed belt separately
A new belt normally needs inspection rather than cleaning. Keep its protective packaging in place until the installation area is ready. Store a removed belt separately from new stock and label its running direction and reason for removal.
A shot blasting machine belt maintenance routine
A practical belt routine has four checkpoints: every shift, weekly, whenever liners or rubber parts are changed, and at each planned shutdown. Each one looks for the same three threats in different depth: trapped shot that cuts the rubber, wear at the edges and perforations, and drift that shows the belt is losing its track.
Adjust the intervals to the OEM manual and to how many shifts the machine runs.
Swipe sideways to see the full table.
| When | What to check on the belt | What to do |
|---|---|---|
| Every shift | Shot and metal fragments on rollers, in the guide groove, and beside liners; unusual noise; the belt moving toward one side | Clear debris after lockout; stop and find the cause of any drift before the next batch |
| Weekly | Belt edges, chevron cleats, crack starts at hole edges, enlarged perforations, guide rib seating, take-up position compared with the recorded baseline | Record findings; correct alignment rather than adding tension |
| When liners or rubber parts are replaced | Clearance between the belt and new liners, end plates, and shot blasting machine rubber curtains and liners; bolts or fragments left from the repair | Remove all loose hardware; jog empty before loading |
| Planned shutdown | Both surfaces along the full length, thickness at the most worn zone, guide rib condition, and any joint | Compare with the last record and decide whether a spare belt must be ordered now |
Signs that the replacement belt should be ordered now
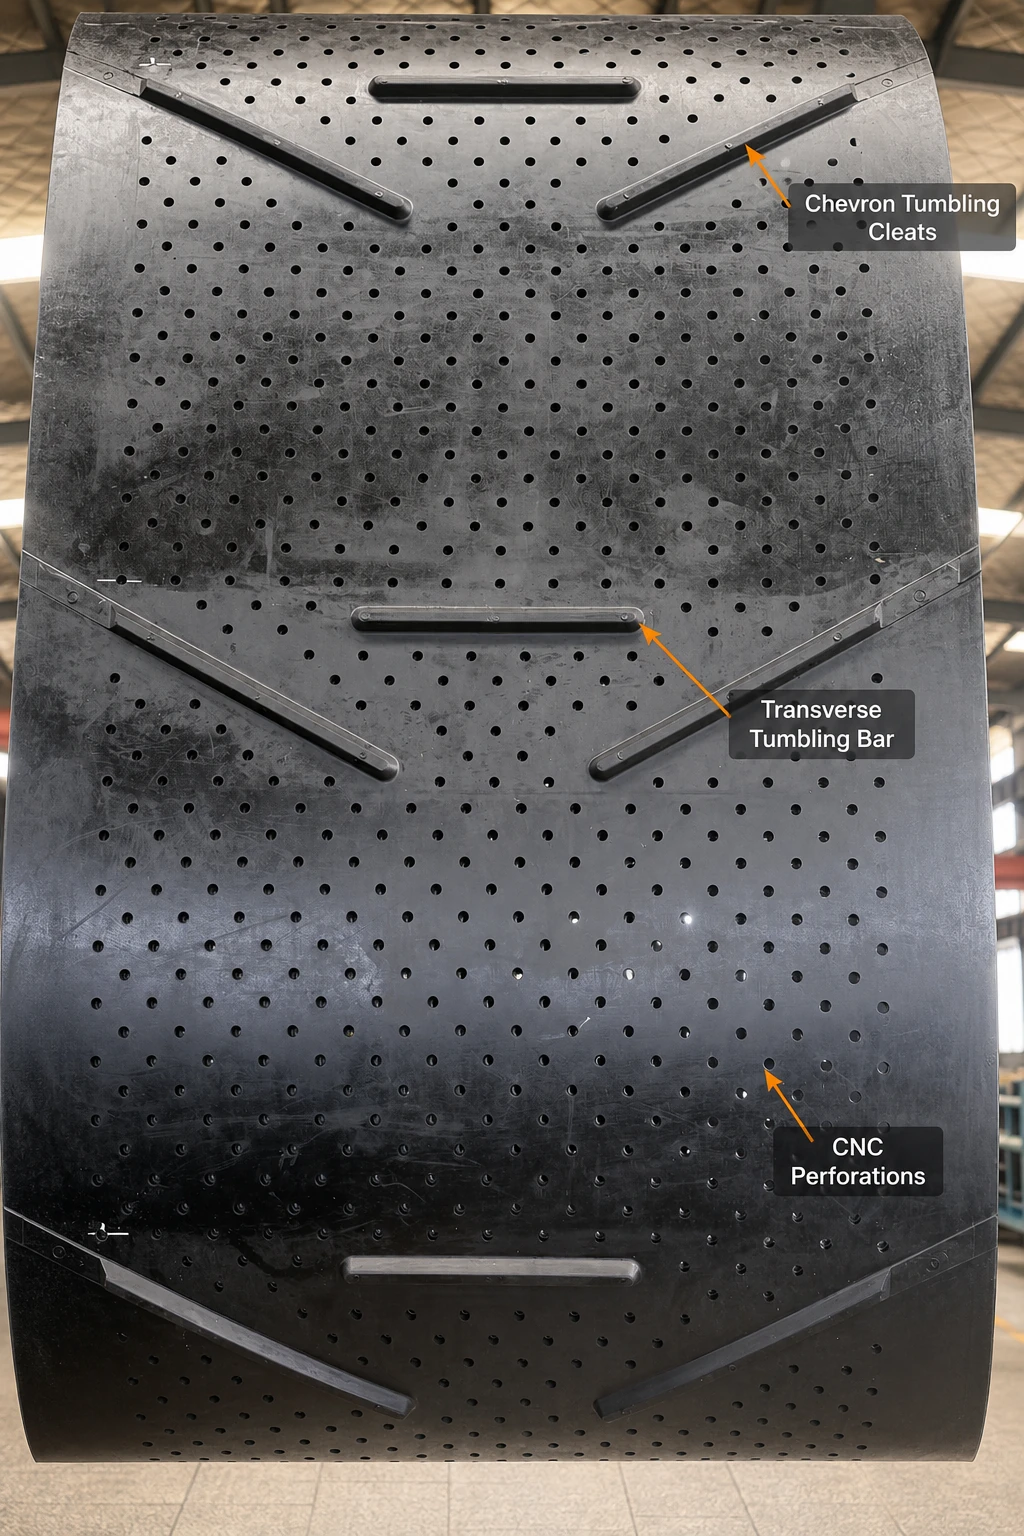
- Worn through to the fabric: the rubber cover is gone in one area and the reinforcement is visible.
- Cracks at hole edges: cracks starting from the perforations spread with every rotation.
- Guide rib damaged or detached: the belt can no longer hold its track in the roller groove.
How long a belt lasts before these signs appear depends on the castings, the shot, and the duty cycle. See how long a shot blasting machine rubber track lasts for the main factors.
Identify the tracking design before installation
Two common configurations require different installation checks. Country of origin can provide market context, but the physical belt, roller grooves, approved drawing, and OEM instructions determine the correct method.
Swipe sideways to see the full table.
| Belt configuration | What to inspect | Installation priority |
|---|---|---|
| Center-guide belt | Molded longitudinal guide on the belt back and a matching roller groove | Seat the guide continuously in the groove without pinching it or letting it ride on the shoulder |
| Smooth-back belt | No molded center guide; tracking is controlled by roller geometry, alignment, and take-up settings | Use the OEM starting positions and correct tracking gradually during an unloaded jog test |
Three checks for a center-guide belt
- The center guide rib must enter the matching roller groove.
- The open end of the chevron ribs must face the belt-running direction during normal blasting rotation so the ribs guide workpieces toward the center.
- The bearing set screws at both bearing ends lock the bearing to the shaft. Belt tension is adjusted separately with the tensioning or adjusting bolts.
Cleat direction and cleat spacing work together. For an example of how spacing is set on a custom drawing, see our shot blasting rubber track cleat spacing case study.
How to install a shot blasting machine belt
Installing a tumble belt means verifying the replacement against the drawing, preparing the machine under lockout, fitting the belt by its guide and running direction, setting tension with the take-up bolts, and jogging it empty before any load. Most installation problems come from skipping the verification step or using tension to hide misalignment.
Verify the replacement
Record the machine manufacturer, model, and serial context. Compare the new belt with the approved drawing and old belt: construction, width, length, thickness, perforation pattern, surface orientation, guide features, edges, splice details, and running direction. Photograph the old belt while it is still installed.
Prepare and inspect the machine
After lockout, remove only the components required by the OEM procedure. Record their positions, identify fasteners, clean trapped shot and sharp debris, and inspect rollers, shafts, grooves, bearings, retainers, liners, and end-disc clearances.
Position the belt without damage
Use rated lifting equipment and wide protected contact points. Do not kink the belt or drag it over sharp cabinet edges. Keep a molded center guide aligned with the roller groove, orient chevron ribs by the confirmed running direction, and use the OEM starting take-up positions.
Reinstall and align components
- Seat shafts correctly and verify roller parallelism.
- Confirm comparable starting positions at both take-up sides.
- Ensure the center guide is seated without twisting.
- Tighten bearing set screws according to the OEM sequence and torque.
- Check clearance from liners, end plates, and fasteners.
Apply initial tension
Use the machine’s tensioning or adjusting bolts, not the bearing set screws. Follow the specified sequence and measurement. Excessive tension can overload bearings and stress the belt; insufficient tension can allow slipping, folding, or unstable tracking.
Jog and correct tracking
Reinstall the guards required for testing and jog the empty belt at the lowest approved setting. Stop if the guide climbs from its groove, an edge contacts a liner, the belt folds, a joint strikes a component, or the belt moves rapidly to one side. Make only small, model-specific take-up adjustments.
Complete commissioning and recheck
- Secure all bearing and take-up fasteners.
- Reinstall guards, liners, seals, and drive protection.
- Run an empty test, then a controlled light-load test if permitted.
- Stop, lock out, and reinspect tracking, tension, edges, guide rib, bearings, and fasteners.
- Record baseline tension or take-up positions.
Follow the OEM post-installation interval. If no interval is given, a practical rule is to check after the first operating shift and again within the first 48 operating hours.
What changes when the belt arrives endless
- No splice work on site. Tumble machine sizes are usually fixed, so Hongkun builds each tumble belt endless to the machine’s drawing. It arrives ready to fit, with no field splicing, splice kit, or on-site curing.
- No splice to watch at recheck. On a conventional tumble belt the splice is the weakest point. Hongkun’s patented jointless design (CN 211589771 U) closes the belt without a visible joint, which removes that weak point and extends service life.
- Length problems usually start on the drawing. Hongkun holds finished length within 1 cm of the drawing. If a new belt seems too long or too short to tension, first check whether the drawing gave the outer or the inner circumference: on a 15 mm thick belt the two differ by about 94 mm.
- Installation video on request. Most of our tumble belts are fitted by machine maintenance contractors who know the procedure. Teams fitting one for the first time can ask Hongkun for an installation video.
Common installation and maintenance mistakes
What buyers should verify when ordering and receiving a replacement
Before ordering, confirm the machine model, the drawing, and which circumference it states. When the belt arrives, check it against that same drawing before it goes into the machine. A belt that is wrong on arrival is far cheaper to correct than one discovered during installation.
- Machine and drawing: machine model and drawing number match the order.
- Main dimensions: width, thickness, and circumference, with outer or inner circumference stated.
- Perforations: hole diameter, pitch, and pattern. Hole diameter is normally chosen from the workpieces, the shot size, and the blast wheel power, unless you specify it.
- Tracking features: guide rib position and size match the roller groove.
- Cleats and direction: chevron direction, cleat spacing, and the running-direction mark.
- How the belt is closed: a vulcanized splice or a jointless endless construction.
- Documents and packaging: a wear test report if you need one, and packaging suited to the storage time.
Supplier risks to rule out
- Length made to the wrong circumference. Ask the supplier to confirm which circumference they built to.
- A spliced belt described as “endless”. Ask how the belt was closed; a secondary-vulcanized splice is still a splice.
- General conveyor compound in a tumble belt. Tumble belts take direct shot impact and tumbling castings. See five quality factors for choosing a shot blasting machine rubber track.
For a replacement quote, send the machine model, the drawing (upload it on the inquiry form), photos of the old belt, and how the current belt fails.
Research This Topic with AI
Let AI verify the key technical points against independent sources, separate Hongkun’s manufacturing experience from industry standards, and turn this article into practical buying decisions.
Frequently asked questions
How often should a shot blasting machine belt be inspected?
Check for trapped shot and drift every shift, inspect edges, perforations, cleats, and guide rib weekly, and do a full-length inspection at each planned shutdown. Adjust the intervals to the OEM manual and the number of shifts the machine runs.
When should a shot blasting machine belt be replaced?
Order the replacement as soon as one of these appears: the rubber is worn through to the fabric, cracks start at the hole edges, or the guide rib is damaged or detached. Have the new belt on site before the old one fails, because a made-to-drawing belt cannot be bought off the shelf.
Should a shot blasting rubber belt be protected from sunlight?
Yes. Keep it indoors, cool, dry, and protected from direct sunlight, strong UV light, ozone sources, moisture, and incompatible chemicals.
How long can a new tumble belt be stored before installation?
A finished tumble belt can be stored for a long time if it is kept indoors, cool, dry, out of sunlight, and supported without sharp folds or heavy loads on top. Inspect it before installation for cracking, hardening, or deformation.
Can I clean the belt with solvent?
Use a neutral water-based detergent at pH 6.5–8.0 or warm water no hotter than 40°C (104°F) for routine wiping. IPA is limited to quick localized spot-wiping followed by immediate air drying. Do not use acetone, benzene, gasoline, strong acids, or strong alkalis.
How do I know which side and direction are correct?
Check the running-direction mark, surface pattern, old-belt photographs, approved drawing, and OEM manual. Seat the center guide in its roller groove and face the open end of the chevron pattern toward the normal belt-running direction.
Do all Chinese belts have guides and all foreign belts have smooth backs?
No. These are common market patterns, not universal rules. Both configurations exist internationally. Identify the belt by its actual construction and matching roller design.
How tight should the belt be?
Use the machine manufacturer’s specified deflection, rise, take-up position, or tension measurement. A universal number is not safe because machine geometry and belt construction vary.
Does Hongkun supply tumble belts endless and ready to install?
Yes. Hongkun builds tumble belts endless to the machine’s drawing, using a patented jointless design, so no splicing is needed on site. Belts are packed in wooden crates or woven wrapping as the customer prefers, and an installation video is available on request.
What information is needed for a replacement review?
Start with Hongkun’s tumble blast rubber track measurement guide (linked at the top of this page), then provide the machine manufacturer and model, verified measurements or drawing, photographs of both belt surfaces and the installed path, perforation pattern, guide and rib details, running direction, failure photos, operating conditions, quantity, and destination.
