Heat-Resistant Conveyor Belts for High-Temperature Materials
Hongkun manufactures heat-resistant conveyor belts for clinker, coke, sintered material, slag, foundry products, fertilizer, cement, metallurgy, and other heated bulk-material applications. Cover compound, carcass, cover thickness, belt speed, and operating arrangement are selected according to the conveyed-material temperature, actual belt-surface temperature, contact duration, particle size, loading depth, cooling conditions, and conveyor design .
Typical High-Temperature Conveying Conditions
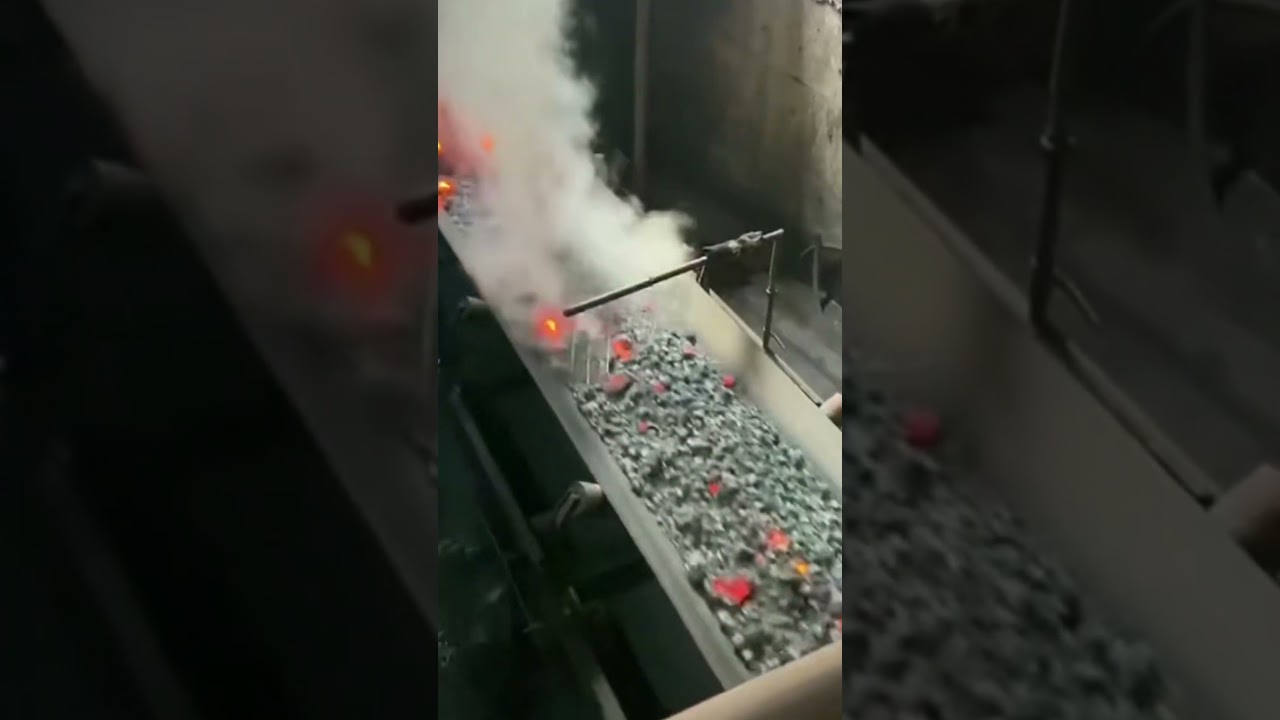
Representative operating conditions include continuously heated bulk material, red-hot particle conveying, and localized hot-lump contact with the belt surface.
High-Temperature Production Line
Belt selection should consider material temperature, loading arrangement, contact time, belt speed, cover thickness, and available cooling.
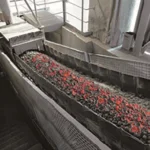
Red-Hot Material Conveying
Compound, cover thickness, carcass construction, loading depth, and operating speed must be matched to the actual thermal load.
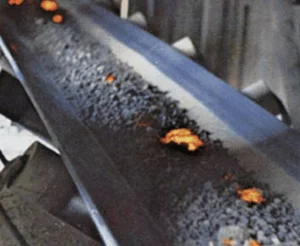
Isolated Hot-Lump Contact
Large or isolated hot particles can produce concentrated thermal stress, localized hardening, cracking, and cover damage.
Heat-Resistant Conveyor Belts for High-Temperature Materials
Available for metallurgy, coking, steel plants, cement production, foundries, glass manufacturing, and other hot-material conveying applications. Final belt construction is selected according to material temperature, belt-surface temperature, particle size, contact time, abrasion, impact, belt speed, and cooling conditions.
Up to 300°C
Application-dependent continuous material temperature
Up to 800°C
Brief exposure under controlled conveying conditions
Up to 1000°C
Isolated hot lumps with limited belt-contact time
Grade references must be confirmed against the applicable product specification, actual belt-surface temperature, and complete operating conditions.
Application-Specific Heat-Resistant Compound
The cover compound is selected to reduce premature hardening, cracking, loss of elasticity, surface deterioration, and adhesion loss during sustained or repeated heat exposure. Heat resistance can also be reviewed together with abrasion, flame, oil, or antistatic requirements.
EP Fabric or Steel Cord Carcass
EP fabric is available for many general and medium-tension systems. Steel cord construction may be selected for long conveyor centres, high working tension, wide belts, heavy loads, and lower elongation requirements. Final carcass selection is based on the conveyor calculation, not temperature alone.
Cover Thickness Reference
Top and bottom cover thicknesses are confirmed from the thermal load, abrasion, impact, pulley diameter, carcass protection, and required service conditions.
Frequently Asked Questions
Temperature selection · Material conditions · Construction · Thermal damage · Quotation
Q
My material temperature is known. Which
heat-resistant conveyor belt grade should I choose?
Material temperature is an important starting point, but it is not sufficient by itself to determine the correct belt grade.
Selection should also consider actual belt-surface temperature, continuous and peak exposure, contact time, particle size, material-layer thickness, belt speed, conveyor length, loading method, return-side cooling, abrasion, impact, and required safety properties.
Provide these operating details so the cover compound, carcass, and cover thickness can be confirmed for the application.
Q
Is the conveyed-material temperature the same
as the belt-surface temperature?
No. The temperature transferred to the belt depends on the material condition and conveyor design.
Two systems carrying material at the same temperature may produce different belt-surface temperatures because of particle size, contact area, layer thickness, belt speed, conveying distance, loading point, ventilation, and return-side cooling time.
When possible, measure the belt surface shortly after the discharge point under stable operation and provide both the material temperature and belt-surface temperature .
Q
Does particle size affect heat-resistant
belt selection?
Yes. Fine material generally creates more continuous contact with the belt surface and may transfer heat differently from larger lumps. Large hot lumps may also cause localized thermal damage and impact at the loading point.
Belt selection should consider:
- Minimum and maximum particle size
- Percentage of fines and large lumps
- Material-layer thickness
- Loading height and impact energy
- Whether hot material accumulates or remains stationary
Q
Why does a heat-resistant conveyor belt become
hard, cracked, or glazed?
Common causes include excessive belt-surface temperature, unsuitable cover compound, prolonged exposure, repeated heating and cooling, insufficient cover thickness, hot-material buildup, impact, and inadequate return-side cooling.
Early warning signs include:
- Loss of cover elasticity
- Surface hardening or glazing
- Fine network cracks
- Localized burnt or brittle areas
- Accelerated abrasion at the loading zone
Photos of the damaged surface and operating information can help distinguish thermal aging from abrasion, impact, mistracking, or splice problems.
Q
What causes cover separation or carcass
delamination?
Delamination can occur when excessive heat weakens the bonding layers between the cover and carcass or between individual fabric plies.
Other possible causes include an unsuitable rubber and bonding system, repeated thermal cycling, excessive flexing, insufficient pulley diameter, severe loading impact, trapped hot material, moisture, edge damage, or incompatible splice materials.
The failure location matters. Separation near the loading point, belt edge, pulley transition, or splice may indicate different root causes.
Q
Should I choose an EP fabric belt or a steel
cord heat-resistant belt?
EP fabric construction is commonly considered for many medium-tension and shorter conveyor applications. Steel cord construction may be considered for long conveyor centres, high working tension, large belt widths, heavy loads, and applications requiring lower elongation.
The decision should be based on conveyor calculations, required strength rating, pulley diameters, take-up travel, splice method, belt width, load, and operating safety requirements, not temperature alone.
Q
Can heat resistance be combined with flame,
oil, or abrasion resistance?
Yes. Heat resistance can be combined with other performance requirements, including flame resistance, oil resistance, abrasion resistance, antistatic properties, and selected chemical resistance.
These properties must be reviewed together because compound changes may affect heat aging, abrasion, elasticity, adhesion, and flame performance.
Provide the conveyed material, oil or chemical type, required safety standard, environment, and fire-risk conditions before selecting the compound.
Q
What information is required for an accurate
quotation and belt recommendation?
Please provide as much of the following information as possible:
- Belt width, total length, and required quantity
- Fabric or steel cord strength rating
- Number of plies, when applicable
- Top and bottom cover thickness
- Continuous and peak material temperature
- Measured belt-surface temperature, if available
- Material name, particle size, and bulk density
- Conveying capacity and belt speed
- Conveyor length, lift, and pulley diameters
- Splice type and applicable technical standard
- Photos, drawings, data sheets, or old belt markings
For replacement projects, photos of the existing damage can help identify whether the previous failure was related to heat, abrasion, impact, tracking, or splice conditions.
What Determines the Actual Thermal Load on the Belt?
Two conveyors carrying material at the same temperature may require different heat-resistant belt constructions. The actual heat transferred to the belt depends on the complete operating conditions, not on material temperature alone.
Material Temperature
The continuous operating temperature, short-term peaks, temperature variation, and frequency of exposure are the starting points for belt selection.
Belt-Surface Temperature
The actual cover temperature is more relevant to rubber aging than the bulk-material temperature alone. Measured belt-surface data is especially valuable for replacement projects.
Particle Size and Contact Area
Fine materials create more continuous surface contact, while large hot lumps may cause localized thermal loading and impact damage at the loading zone.
Material Layer Thickness
A deeper or more compact material bed can retain heat and increase contact time. Uneven distribution can also create hotter areas across the belt width.
Belt Speed and Contact Time
Belt speed, conveyor length, loading position, and discharge point determine how long the hot material remains in contact with the cover.
Cooling and Ambient Conditions
Return-side cooling, ventilation, ambient temperature, conveyor enclosure, water-cooling systems, and downtime between cycles all influence heat dissipation.
Common Applications and Heat-Related Failure Signs
Heat-resistant conveyor belt selection should consider both the conveyed material and the failure pattern of the existing belt. Material condition helps determine the required compound and construction, while wear and damage signs can reveal the actual operating problem.
Common Hot-Material Applications
Representative materials requiring heat, abrasion, impact, or combined performance review.
Cement Clinker
Hot clinker and kiln-discharge conveying where heat, abrasion, dust, and material-layer thickness must be considered together.
Coke and Sinter
Coke, sinter, and metallurgical bulk materials with abrasive particles and repeated heating and cooling cycles.
Steel Slag
Hot slag and steelmaking materials involving sharp particles, concentrated heat, loading impact, and localized cover damage.
Foundry Materials
Foundry sand, casting residues, and hot process materials requiring resistance to thermal aging, cracking, and abrasion.
Hot Glass Materials
Glass cullet and process materials where sharp edges, impact, concentrated hot spots, and cover thickness require careful review.
Ash and Metallurgical Materials
Hot ash, ore, coke, and other bulk materials used in power generation and metallurgical processing.
Common Heat-Related Failure Signs
Damage patterns can help separate heat problems from abrasion, impact, tracking, flexing, or splice issues.
Surface Hardening
The cover gradually loses elasticity and becomes stiff after prolonged heat exposure or use of an unsuitable compound.
Network Cracking
Repeated heating, cooling, and belt flexing may produce fine cracks that expand during continued operation.
Cover Delamination
Thermal aging, impact, excessive flexing, splice conditions, or unsuitable pulley diameters may weaken cover-to-carcass adhesion.
Localized Burning
Isolated hot lumps, trapped material, material buildup, or a stopped conveyor may create concentrated thermal damage.
Loading-Zone Wear
Heat, impact, and abrasion can combine at the loading point, causing faster cover loss than on the rest of the belt.
Edge or Splice Damage
Mistracking, hot fines, structure contact, or incompatible splice materials may accelerate edge wear or separation around the splice.
Already Experiencing Belt Cracking, Hardening, or Delamination?
Send photos of the worn cover, loading zone, belt edges, return side, and splice area, together with the material temperature and operating conditions. The damage pattern can help identify whether the main cause is heat, abrasion, impact, mistracking, flexing, or adhesion failure.
Standards and Performance Options for Heat-Resistant Conveyor Belts
Heat-resistance testing, belt construction, additional compound requirements, and inspection scope are confirmed according to the approved technical specification and customer requirements.
| Standard or Requirement | Main Scope | Application and Confirmation |
|---|---|---|
| ISO 4195 | Heat resistance of rubber conveyor belt covers | Used as a reference for evaluating changes in rubber-cover properties after heat exposure, including hardness, tensile strength, and elongation at break. Heat-Resistance Testing |
| ISO 15236 Series | Steel cord conveyor belt construction | Used as a structural reference for selected steel cord conveyor belt dimensions, mechanical requirements, construction, and related technical parameters. Steel Cord Reference |
| Customer-Specified Standards | DIN, ISO, JIS, GB, HG, or project-specific requirements | The required standard edition, test method, performance values, documentation, and inspection scope should be stated in the purchase or technical specification. |
| Combined Performance Options | Heat + abrasion, flame, oil, antistatic, or other requirements | Additional properties can be reviewed together with heat resistance. The conveyed material, operating temperature, required test method, safety category, and acceptance values must be confirmed before compound selection. Application-Specific Compound |
Important: the standards and options listed above are available reference frameworks, not automatic claims of compliance for every belt. Compliance with a specific standard is confirmed only when the applicable edition, test methods, required values, inspection scope, and documentation are included in the approved technical agreement.
Steel Cord Carcass References for Heat-Resistant Conveyor Belts
Reference structural parameters for selected ST630–ST2000 steel cord belt constructions. Final strength rating, cord layout, cover thickness, belt weight, heat-resistant compound, and splice design must be confirmed from the conveyor calculation and operating conditions.
| Carcass and Structural Parameter | ST630 | ST800 | ST1000 | ST1250 | ST1600 | ST2000 |
|---|---|---|---|---|---|---|
| Nominal Longitudinal Tensile Strength Minimum belt strength, N/mm | 630 | 800 | 1000 | 1250 | 1600 | 2000 |
| Reference Maximum Steel Cord Diameter mm | 2.9 | 3.4 | 4.0 | 4.5 | 5.0 | 5.7 |
| Reference Steel Cord Pitch Centre-to-centre spacing, mm | 10.0 | 10.0 | 12.0 | 12.0 | 12.0 | 12.0 |
| Approximate Number of Cords per Metre Reference quantity, pcs | 99 | 99 | 82 | 82 | 82 | 82 |
| Reference Minimum Cover Thickness Top / bottom cover, mm | 5.0 / 5.0 | 5.0 / 5.0 | 6.0 / 6.0 | 6.0 / 6.0 | 6.0 / 6.0 | 6.0 / 6.0 |
| Nominal Belt Weight Reference Based on 6 mm top + 6 mm bottom cover, kg/m² | 21.8 | 23.1 | 25.3 | 26.8 | 28.5 | 31.0 |
Technical and Customization Notes
- Cover thickness: the minimum cover values are structural references. For heat-resistant service, the top and bottom cover thicknesses may be increased or redistributed according to temperature, abrasion, impact, pulley diameter, carcass protection, and required service conditions.
- Belt weight: the listed weight values use a common 6 mm + 6 mm cover basis for comparison. Actual belt weight changes with belt width, cord construction, cover thickness, rubber density, breaker layers, edge design, and manufacturing tolerance.
- Heat-resistant construction: steel cord strength does not determine heat resistance by itself. The cover rubber, skim compound, cord adhesion, thermal-aging performance, and splice materials must be selected together.
- Final confirmation: cord diameter, cord pitch, cord quantity, cover thickness, safety factor, pulley diameters, take-up arrangement, splice design, and applicable standard should be confirmed before production.
Standards notice: steel cord conveyor belt construction can be manufactured according to the confirmed DIN, ISO, GB, JIS, or customer-specified requirements. A belt should only be described as compliant with a specific standard when the standard edition, construction, test methods, performance values, inspection scope, and required documentation are included in the approved technical agreement.
